Specification and material
Before fabrication we establish the medium, pressure and temperature, material grades, joint geometry, dimensions, installation location and required quality.
 PROJECTEnquire ↗
Technology / Fabrication, installation and overhaul
We offer comprehensive metal and plastic welding, from joint design and process preparation through fabrication, installation, repairs and inspection. The process, material and documentation scope are tailored to the product and its service conditions.
Operating context
We address structural and process piping, welded assemblies, corrosion-resistant components and plastic process equipment. Alongside conventional arc and plastic-welding methods, we develop individual solutions for special materials and processes. A required welding procedure can be added and qualified for the project.
Engineering priorities
Before fabrication we establish the medium, pressure and temperature, material grades, joint geometry, dimensions, installation location and required quality.
Each joint type is assigned a suitable welding procedure and personnel qualification. Assessment covers material groups, process, thickness, diameter, position, filler and the other conditions of the applicable record.
We prepare joint surfaces, fit-up and component identification; weld maps and material-record traceability are maintained as specified. Plastics work addresses cleanliness, system compatibility and fusion-cycle conditions.
Access to joints may change after assembly. The inspection plan therefore links visual and other non-destructive examinations to fabrication or repair stages and final verification.
For automated welding, we coordinate joint location, clamping, reach and access for the torch or spot-welding gun. Path design and weld sequence are checked against fixture geometry and part transfers. Sample trials follow the specified welding procedure and inspection plan.
Before engineering
Agreed with the proposal
The actual scope and acceptance criteria depend on the application and contract.
Metal and thermoplastic joining
The required product defines the scope of supply. The specific procedure, equipment and qualifications are established during project preparation.
Carbon and low-alloy steels for structures, piping and process assemblies. MMA, MAG or TIG is selected for the joint, access and production scope.
Joining of austenitic stainless steels, duplex steels, selected nickel alloys and aluminium materials. Preparation covers suitable filler, shielding and thermal conditions.
For repeat production or larger sections, we develop the mechanisation approach, run sequence and joint preparation. Submerged-arc or plasma processes can also be addressed for a specific project.
Laser welding is assessed for suitable materials and component geometry. Preparation reviews fit-up accuracy, access and required weld quality, with a trial joint where needed.
PE, PP and PVDF piping systems are specified for the medium, temperature and pressure. The scope includes butt fusion and socket fusion, with other suitable jointing methods selected for the system.
Extrusion or hot-gas procedures are developed for sheet fabrications, vessels, troughs, ducts and repairs. Preparation distinguishes PE, PP, PVC and PVDF, filler material, surface condition and weld geometry.
Electrofusion fittings are selected for compatibility with the particular piping system. Work covers surface preparation, restraint, execution of the fitting-specific cycle and inspection of the completed joint.
For atypical products, we can assess resistance, stud, friction, ultrasonic, beam or specialised plastic joining. The proposal addresses process suitability, required equipment, a test specimen and how the result will be verified.
Engineering the joint
We prepare the procedure specification, its technical variables, links to qualification and handover documentation. Required approval and any tests are determined by the product and contract.
01
Preparation distinguishes both joint materials, thicknesses, diameters and weld-preparation geometry. Butt, fillet, lap, socket and custom joints can be addressed.
02
The root, fill and cap sequence, process, filler, shielding gas and required parameters are specified. Plastic joints use the appropriate welding or fusion cycle.
03
Process preparation can include weld length and volume take-offs and estimates of filler, gas and working time for project costing.
04
Documentation connects the procedure with the applicable qualification record, inspection plan and responsible approval. The draft is completed following technical review or a qualification test.
05
Welding specifications can be prepared in Czech, English or German. A common input set helps keep technical information consistent across language versions.
We include procedure development, a trial assembly, testing and qualification coordination in the proposal. The required scope is defined for the application before production begins.
Discuss the welding scope ↗Supporting qualification resources
A WPQR records procedure qualification, a WPS specifies the production procedure, and an individual certificate defines the welder’s qualification. Preparation brings these records together for the particular joint. These examples describe existing records; the offered scope can be extended through technical preparation and qualification for the new work.
WPQR 533/01/2023
Fabrication of welded assemblies, supports, frames and pipework within the material and joint-design scope.
The procedure is selected for joint geometry, thickness, required mechanical properties and inspection conditions.
WPQR 05.653.478 / WPS F47
Stainless-steel piping and process components with requirements for root quality and the post-weld surface condition.
Root shielding, filler material, cleaning requirements and weld examination are specified before fabrication.
WPQR 401/02/2018
Duplex-steel piping and process components, using a procedure selected for the specific material and thermal conditions.
Butt-joint applicability depends on more than the material grade: filler, heat input, position and joint configuration are also considered.
WPQR 401/1/2018
Special corrosion-resistant components, with the procedure selected for the alloy, service medium and joint.
The dimensions apply to the two members of the specified fillet joint; the manufacturing drawing defines the quotation scope.
Individual basic-course certificate ZK 11 P 3
Workshop and site joining of PE piping, including end preparation, alignment and a system-specific welding cycle.
Where an advanced qualification is required, the corresponding qualification record and procedure conditions are established in advance.
Individual basic-course certificate ZK 16 P 3
PE pipe connections and repairs using electrofusion fittings, including surface preparation, joint restraint and recording of the fusion cycle as specified.
Material compatibility and dimensions are checked against the system manufacturer information; an advanced qualification is documented where required.
Individual basic-course certificate ZK 15 P 2
Fabrication and modification of PP piping, connections to valves and process equipment, and agreed tests of the completed assembly.
Procedure, joint preparation and welding conditions are selected for the material and system; advanced qualification is arranged where required by the application.
Individual thermoplastics welder qualification under EN 13067
Welding of PE plate components and process assemblies, including groove preparation and control of preheating and extrusion.
Joint geometry, product design conditions and required procedure verification are established before fabrication.
Relevant experience
Project 526 · Handling & automation
Installation location: Mladá Boleslav, Czechia · 2023–2025
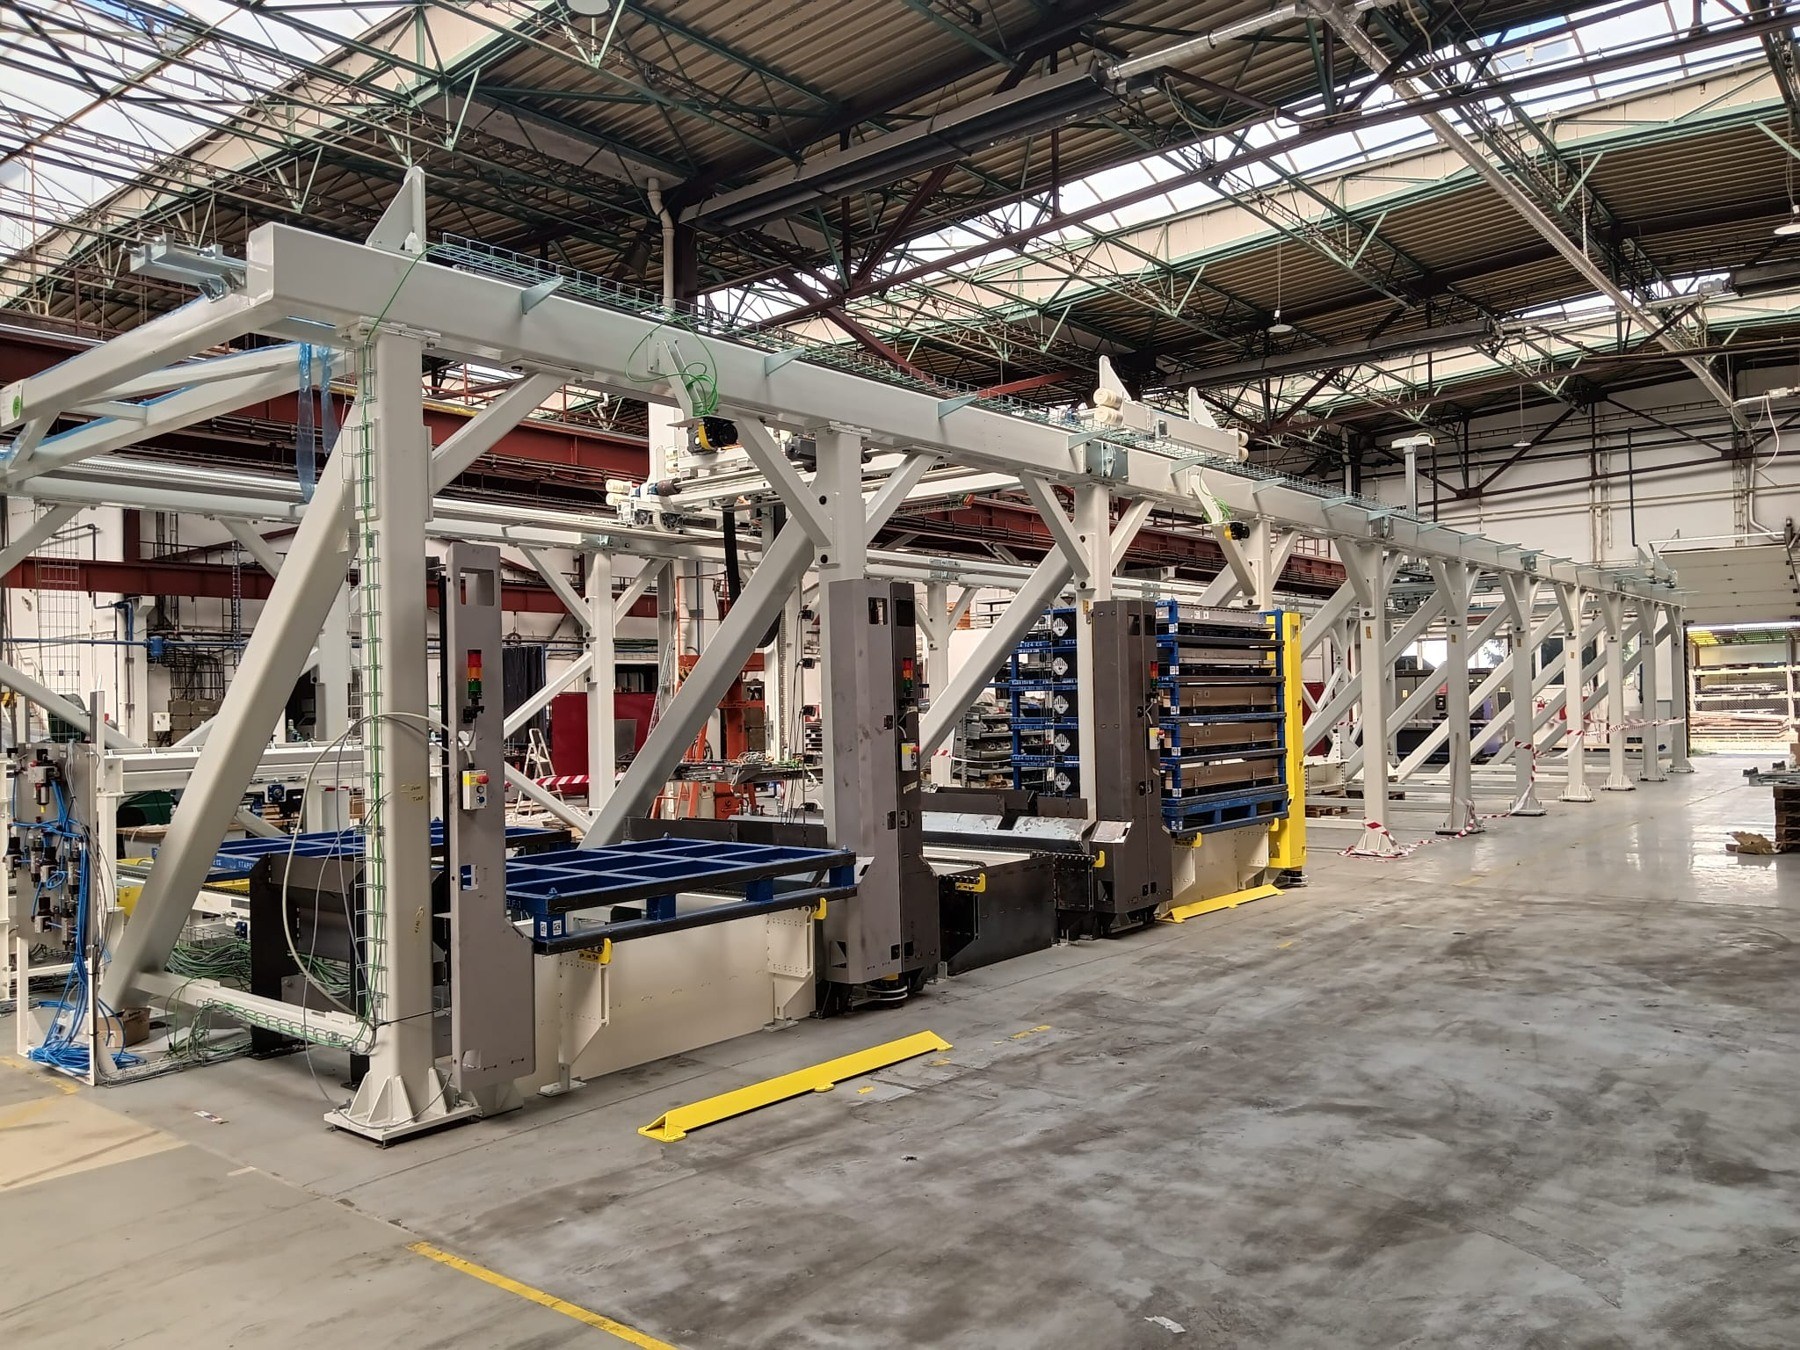
Two gantry manipulators, conveyor interfaces and battery flow control for automotive production in Mladá Boleslav. The reference covers handed-over engineering and partial delivery stages.
Broader project portfolioEngineering and partial delivery stages
Project 667 · Process plant upgrades
Installation location: Lovosice, Czechia · 2024
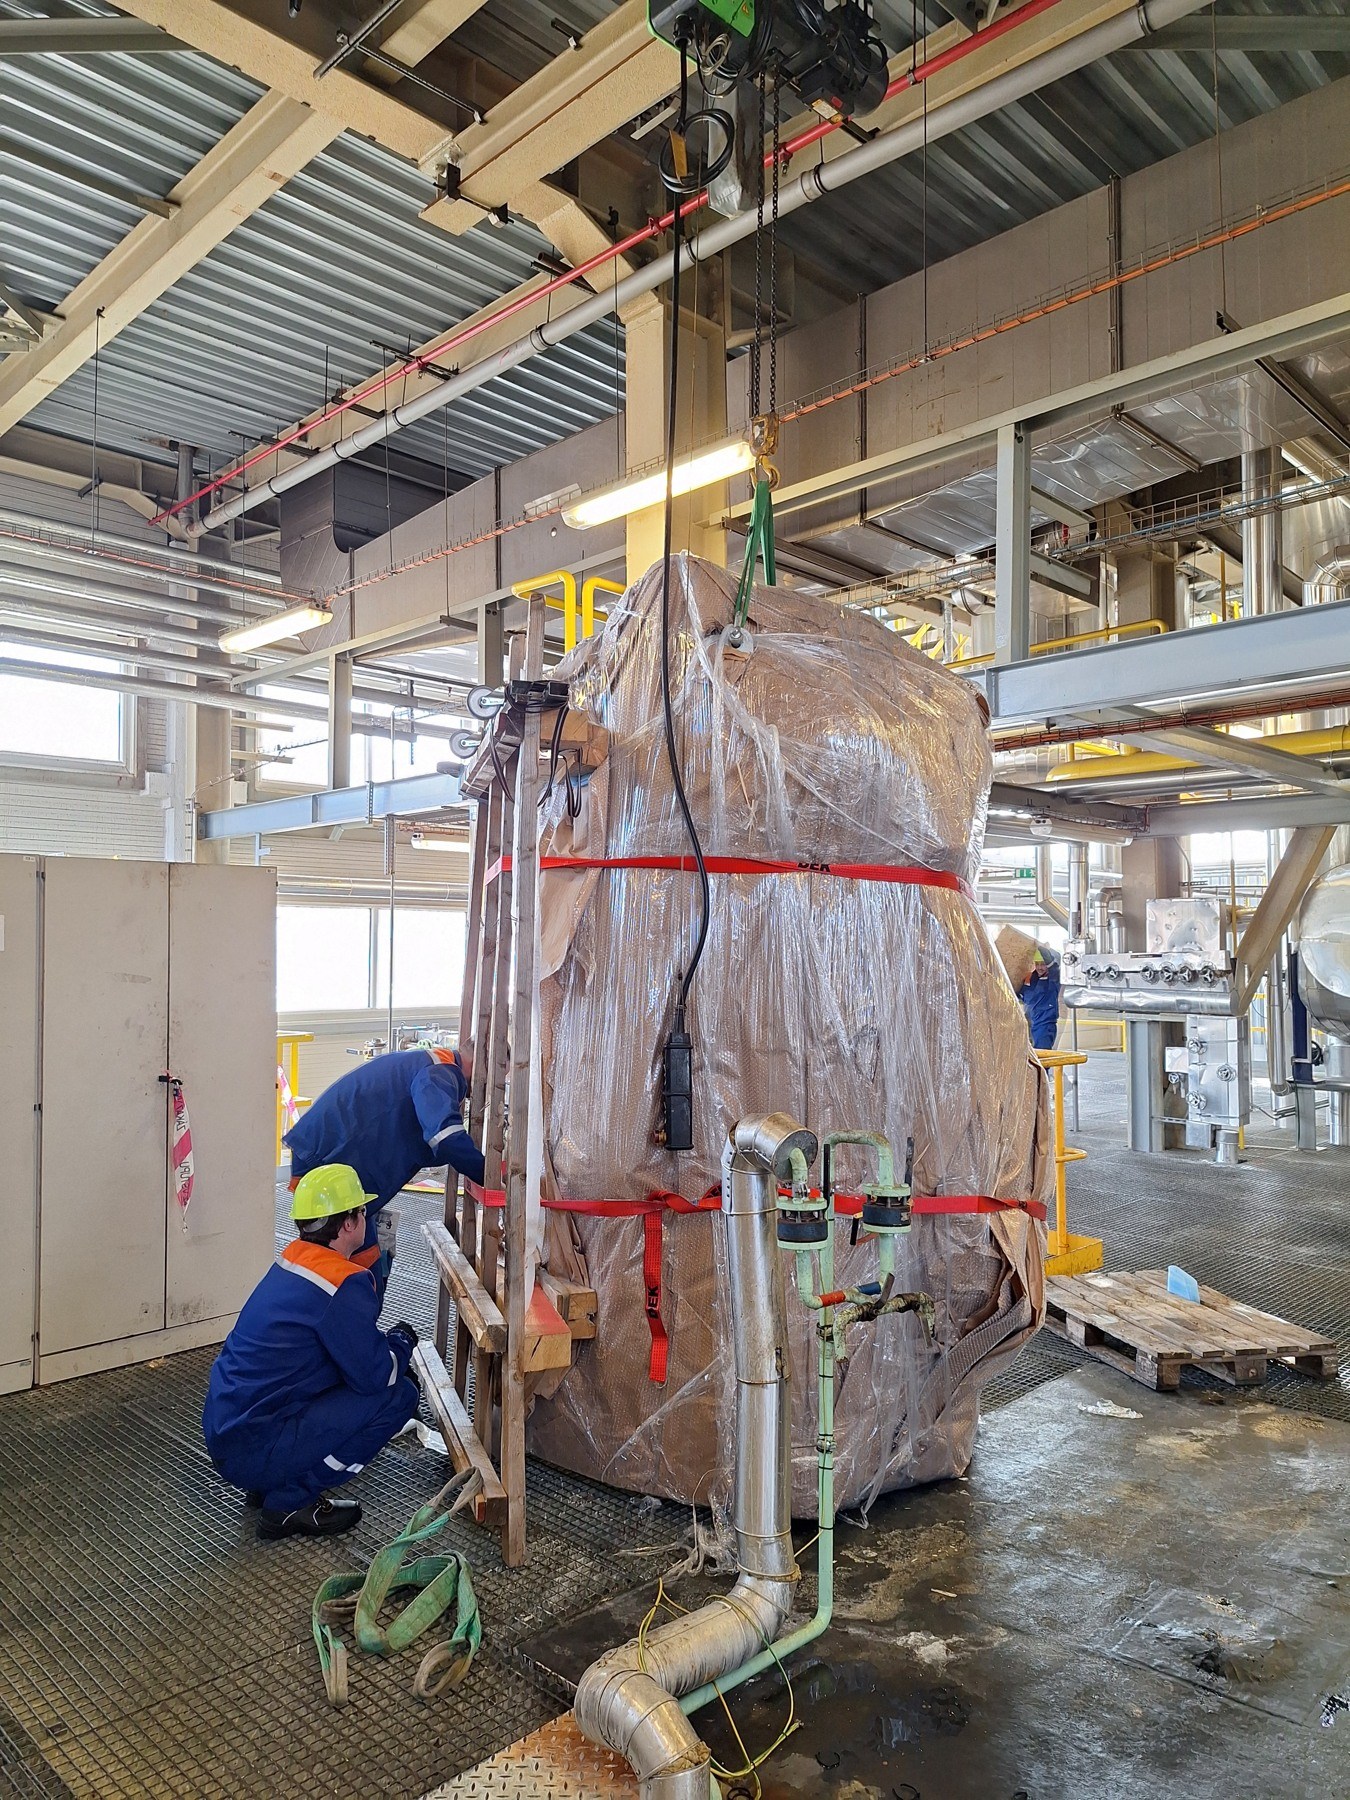
Replacement of a 3.9 m³ reactor on a +6 m platform, including agitator assembly and modification of 15 pipe runs.
Broader project portfolioEquipment replacement, installation and connection
Project 741 · Process plant upgrades
Location: Pardubice, Czechia · 2025
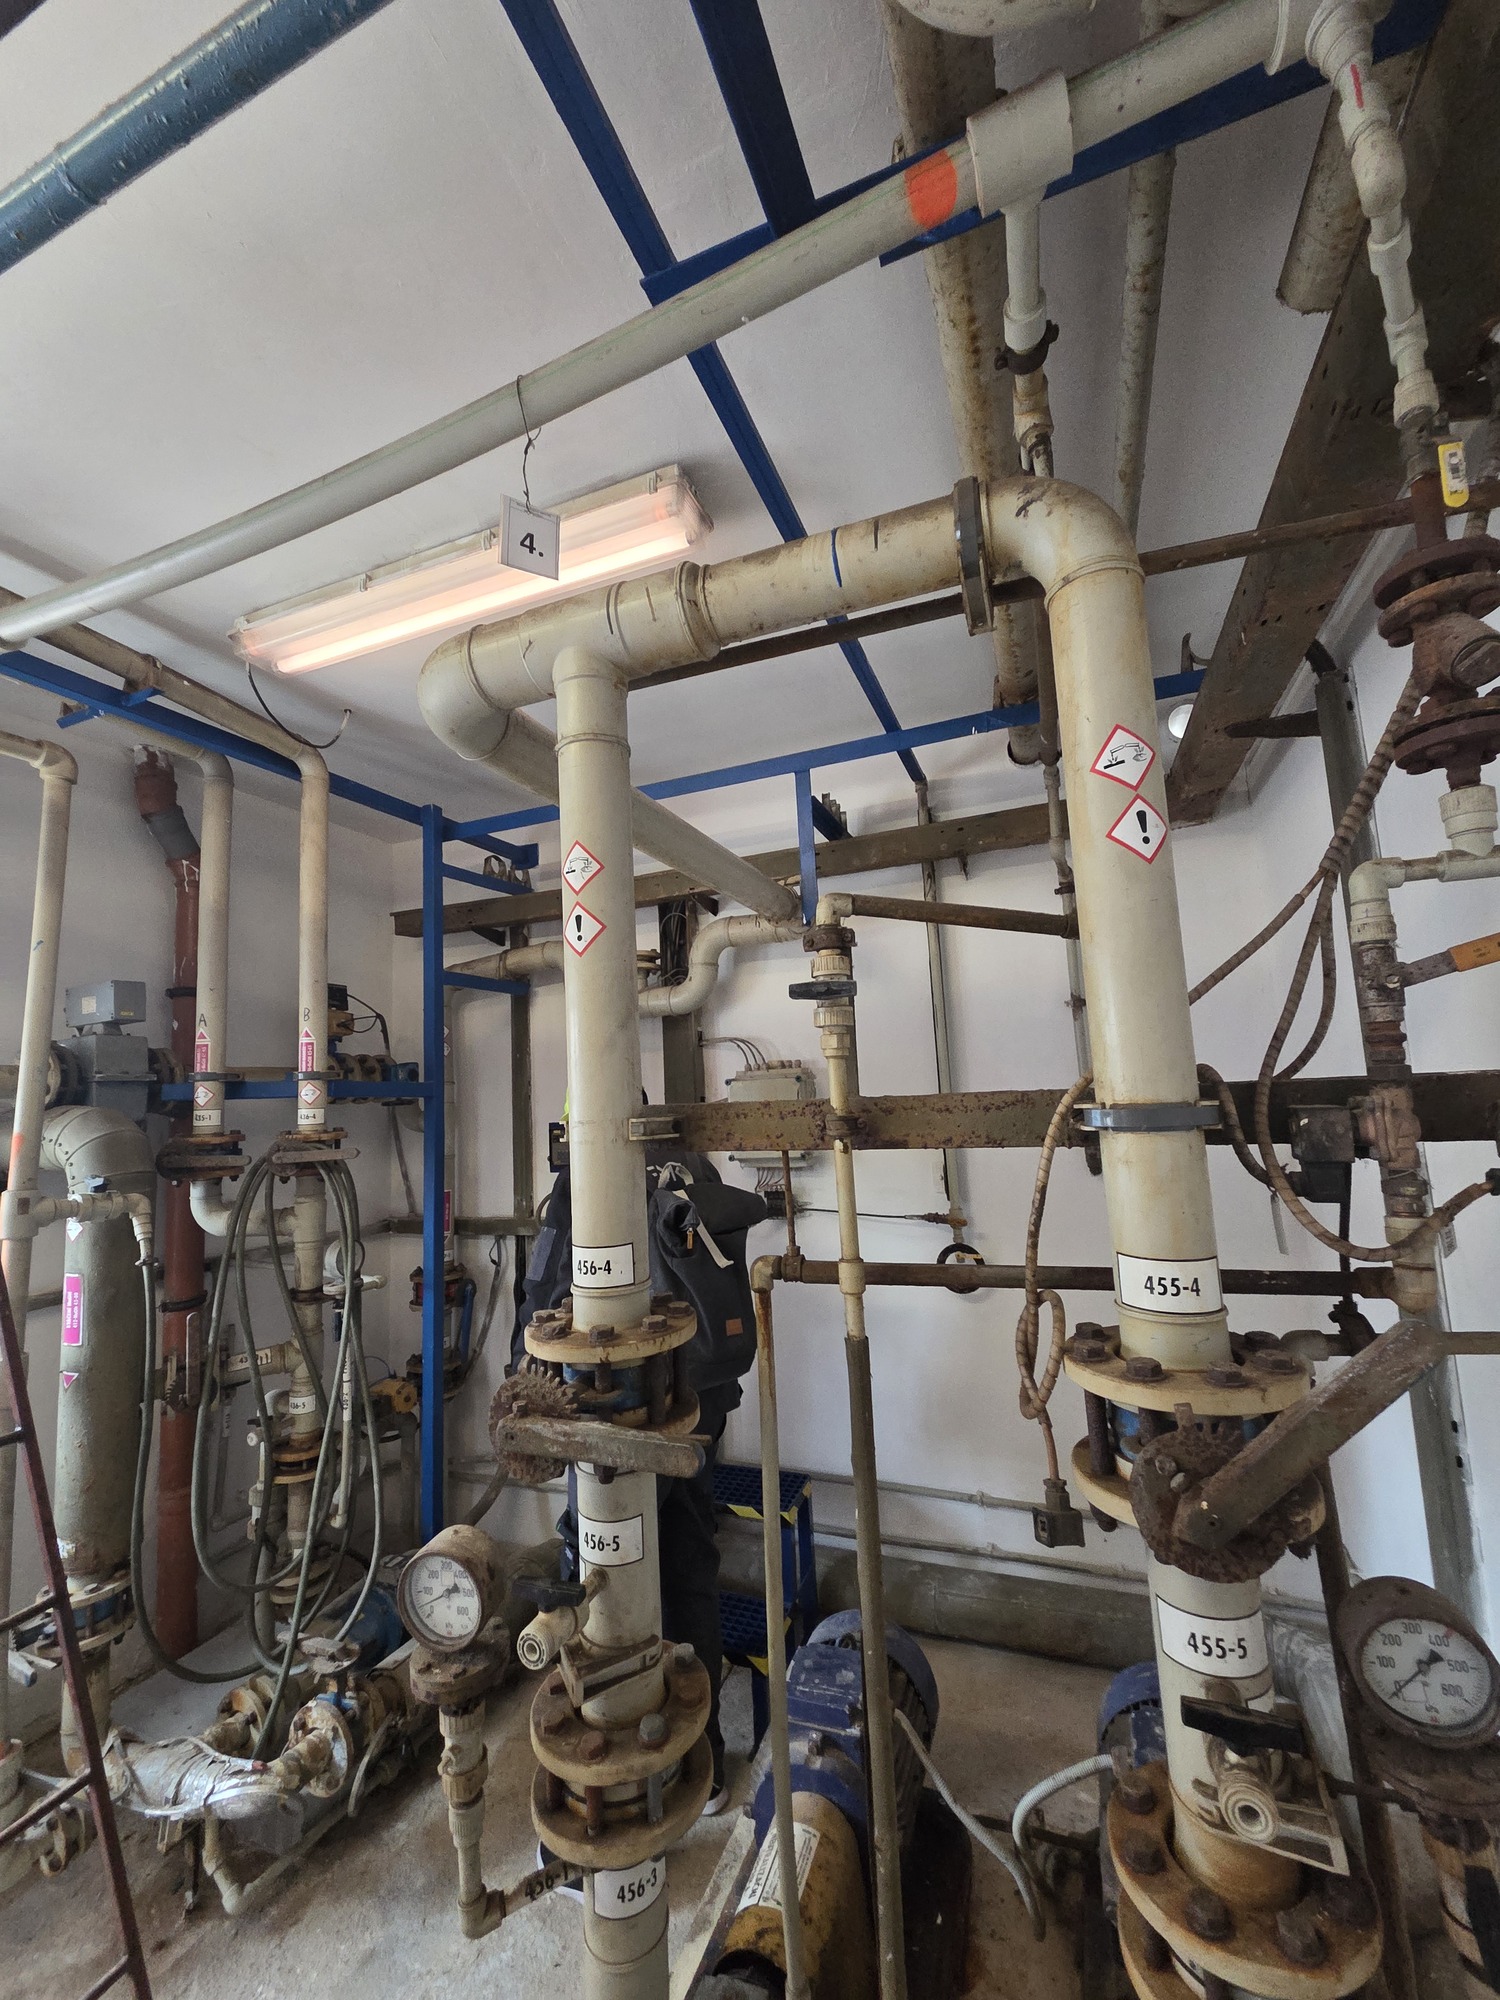
Handed-over stages of temporary HCl storage: engineering, installation, connection and operator training.
Broader project portfolioPartial engineering and installation stages
Connected disciplines
Related technologies
Your next project
Send your drawings, operating parameters or a short description of the change you need. We will review the technical interfaces and propose the next steps towards a quotation, clarifying any missing information with you.
Discuss your requirements ↗Prepare a technical brief →+420 731 771 147info@emkoproject.cz